What Is Rework in Manufacturing? Causes, Costs, and Reduction
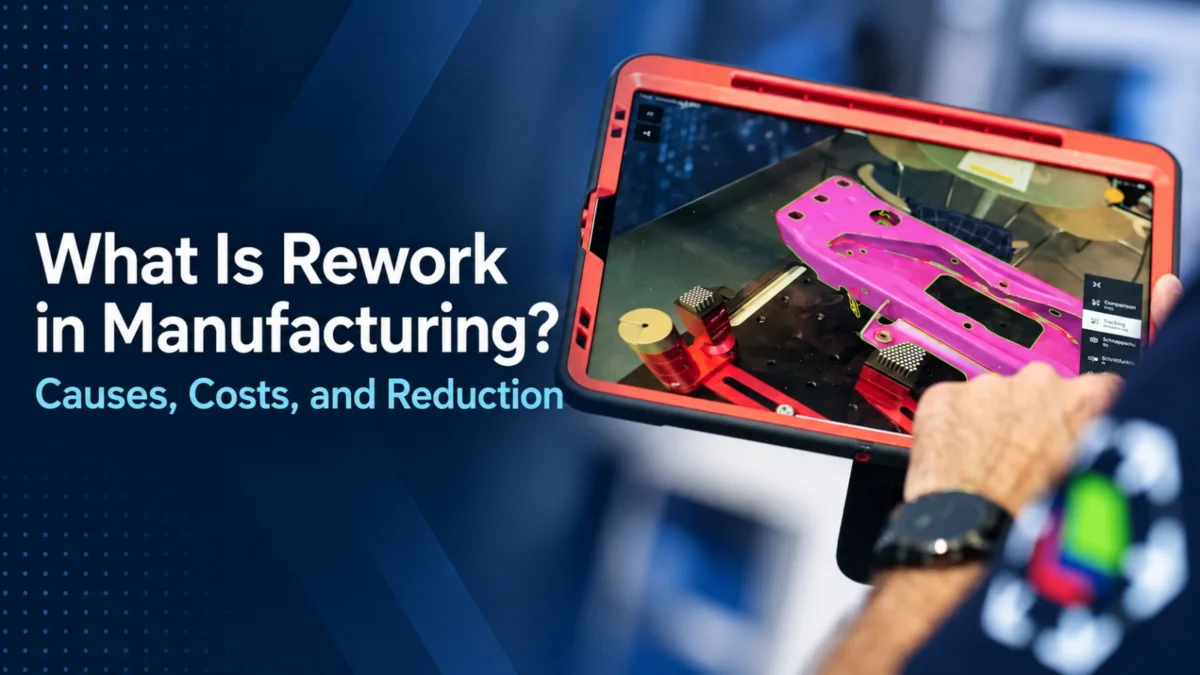
Rework in manufacturing is the process of correcting a part or product so that it meets its requirements, instead of accepting it or discarding it. It can involve machining, re-welding, re-assembly, cleaning, or replacing a component. Rework takes time and resources, and it often disrupts the production schedule. Reducing rework often depends on addressing root causes and identifying nonconformances as early as practical in the production process. AR-guided visual verification can support this by helping teams compare the physical assembly with its expected CAD-based reference before it moves to the next operation.
What is rework in manufacturing?
Rework is any corrective action taken on a part or assembly that does not yet meet the defined requirements. The part is brought back into conformance through an additional operation, rather than being scrapped or accepted as it is. Rework is common in welding, assembly, machining, and finishing, where a missing component, incorrect position, or process variation may need to be corrected. Because rework consumes labour, machine time, and material, it is usually tracked as a cost and a signal of process instability.
What is the difference between rework, repair and scrap?
Rework, repair, and scrap are different responses to a nonconforming output. Rework brings a part back to its original requirements through a defined corrective process. Repair restores a part to a usable condition, which may not match the original specification in every respect, and it usually requires a formal engineering decision. Scrap means the part is discarded because it cannot be made conforming. Quality management systems typically require nonconforming outputs and the actions taken in response to them to be controlled and documented. Where ISO 9001 is referenced, the applicable requirements should be verified against the current standard.
What causes rework on the production floor?
Rework is often caused by a combination of factors. Common causes include incorrect or missing components, parts loaded in the wrong orientation, unclear work instructions, fixture or tooling problems, and process variation in welding or machining. Errors may also originate upstream, where a design or supplier issue is not discovered until the part reaches assembly. Identifying the root cause is important, because correcting the symptom alone will not prevent the same rework from recurring.
How does the rework process work?
A typical rework process begins with the identification of the nonconforming condition, followed by a decision on whether the part can be corrected. The issue is documented, the responsible team is informed, and the corrective operation is defined. After the rework, the part is checked against the requirements and released or routed for further action. Good practice includes recording the reason for rework, the operation performed, and the result of the verification, so that the data can be used for improvement.
How do you track rework and its costs?
Tracking rework starts with a clear definition of what counts as rework and a consistent way of recording it. Teams typically log the part or batch, the nonconformity, the operation that caused it, the corrective action, and the time and material used. These records can then be analysed by station, shift, product, or supplier to identify patterns. Cost tracking usually includes labour, machine time, material, and the effect on delivery schedules. Clear records also support traceability, which becomes important when a rework affects several parts or a customer requirement.
How can earlier visual verification help reduce rework?
Visual verification can help reduce rework by catching errors before a part moves to the next operation. When operators can compare a physical assembly with its CAD reference, visual verification can help identify missing, extra, or visibly misplaced features at the stage where the inspection is performed. SuPAR App can provide CAD-based visual guidance and structured inspection checkpoints on the physical part, while SuPAR AI can support automated visual verification of suitable repetitive inspection targets, such as holes, spot welds, and studs, under defined operating conditions. Earlier identification of a visual nonconformance can help reduce the amount of correction required later in the process, depending on the application, inspection scope, and production workflow.
How do you choose a rework reduction strategy?
A rework reduction strategy should start with the data. Teams review the most frequent and most costly rework causes, identify where in the process they occur, and determine whether the root cause is design, process, tooling, material, or human factors. Options include poka yoke methods, clearer work instructions, fixture improvements, supplier controls, and visual verification at key stations. The strategy should be tested on a limited scope, measured over a defined period, and adjusted based on the results.
Frequently Asked Questions
Is rework considered waste in Lean manufacturing?
Yes. In Lean thinking, rework is treated as a form of waste because it consumes resources without adding value to the customer. Lean programmes aim to reduce rework by addressing its root causes, rather than accepting it as a normal part of production.
Who approves rework on a production line?
Rework decisions are usually made by quality engineering, sometimes with input from manufacturing engineering or the customer, depending on the nature of the nonconformity. The approval process should be defined in the plant’s quality procedures and recorded for each case.
How does rework affect part traceability?
Rework can complicate traceability because the part may have been processed more than once and may have been handled differently from the standard route. Records should show the rework operation, the person or station responsible, and the verification performed, so that the part’s history can be reconstructed if needed.
Can reworked parts be shipped to the customer?
Reworked parts can be shipped if they meet the defined requirements and the customer has accepted the correction method where required. Some customers have specific rules about rework, so teams should check the applicable contracts and quality agreements before releasing reworked material.
What is a rework rate and how is it calculated?
A rework rate is commonly calculated as the number of parts requiring rework divided by the total number of parts produced in the same period, often expressed as a percentage. The definition should be agreed within the organisation, including whether a part counted for rework is counted once or each time it is corrected, so that the metric is consistent over time.